Short answer: RepaKORR was a German research project, funded by the Federal Ministry of Education and Research (BMBF) and coordinated by Muehlhan, that developed repair concepts for anticorrosive coatings on offshore wind structures. It analysed why coatings fail, qualified repair coatings with accelerated ageing, impact and abrasion tests, and defined a five-step field-repair sequence in which mechanical surface preparation with a rotating bristle tool is a central step.
This summary covers who ran RepaKORR, what its damage analysis found, the offshore field-repair sequence it set out, the mechanical tests used to qualify repair coatings, and what the results mean for surface preparation on wind and renewable energy assets.
The project
RepaKORR (“Repair systems and concepts for anticorrosive coatings of offshore wind structures”) was funded by the German Federal Ministry of Education and Research (BMBF, project 03X3570A) and coordinated by Muehlhan AG. It brought together Muehlhan AG (application procedures), Fraunhofer IFAM (qualification and verification; temporary protection), Sika Deutschland (repair materials), AirRobot (inspection drone), Corroconsult (damage assessment), RETC (regulatory and environmental issues) and WeserWind (design and logistics), with turbine maker Senvion as an associated partner. Fraunhofer reported that the concepts were to be ready for implementation by March 2016; results were presented in industry sessions and at conferences in 2016–2017.
The motivation was cost. According to Fraunhofer, repairing coatings offshore can cost several thousand euros per square metre, against roughly €20–30 per square metre for comparable work onshore — so a repair that fails early is very expensive. Alongside the repair procedures, the project worked on temporary protective films for the interval between surface preparation and coating, and on drone-based inspection.
Why offshore coatings fail
Analysing coating damage on platform-type structures, the project attributed failures roughly to: mechanical damage (~30%), unfavourable design (~30%), insufficient coating (~24%), welding (~11%) and environment (~5%). Much of the mechanical and design-related damage occurs in exactly the places that are hardest to inspect, blast-clean, paint and repair — corners, openings, connections and areas with poor access, as also recognised in ISO 12944-3.
The offshore field-repair sequence
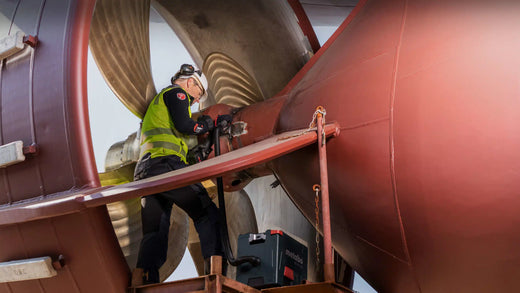
The project set out a five-step field-repair procedure for offshore structures, carried out largely by rope-access technicians:
- Access & protection / housing — reach and wrap external areas, and access internal sections.
- High-pressure water washing — remove dirt, impurities and soluble salts (notably chlorides) from the substrate — see why soluble salt contamination causes coating failure.
- Blast-cleaning — wet blasting in the atmospheric, splash and tidal zones, followed by fine cleaning.
- Power tooling — coating removal and profiling with a rotating bristle brush, de-rusting with a grinder, scale and rust removal with a needle hammer, and weld-seam cleaning with a power brush.
- Paint application — by roller, cartridge or brush.
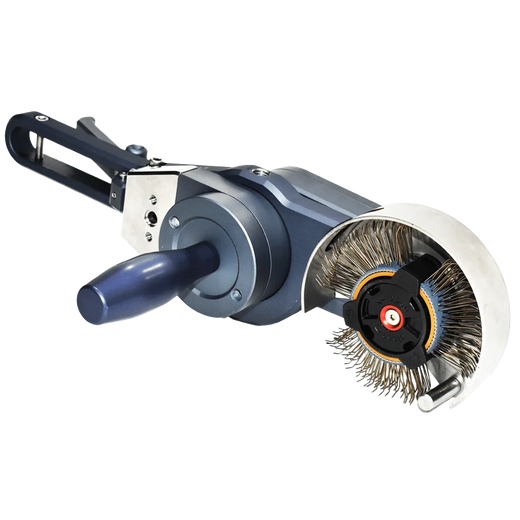
Step 4 is where mechanical surface preparation earns its place: in confined, access-limited and splash-zone areas where wet blasting is impractical, a rotating bristle tool removes the failed coating and generates the anchor profile in one grit-free step — the same principle behind the Bristle Blaster®. The MontiPower® Bristle Blaster® Pneumatic, fully air-driven and evaluated under ATEX for zone 1 gas and zone 21 dust, produces cleanliness comparable to Sa 2½ with a 65–85 µm Rz profile in documented tests on standard steel; results vary with steel grade, rust grade, belt and technique. For localised damage, see spot repair preparation.
Qualifying the repair coatings
Fraunhofer IFAM subjected candidate repair coatings to accelerated ageing and to the mechanical tests used for certification, including:
- Impact strength (falling weight, ASTM G14): greater than 3.4 J for non-deck areas and greater than 5.6 J for decks and the boat-landing splash zone.
- Abrasion resistance (Taber, ASTM D4060): coating-thickness loss under 50 µm per 1,000 cycles.
Together with the ISO 12944 corrosivity categories, these criteria define whether a repair system applied under offshore field conditions can be expected to last. Repairs below the waterline are a separate challenge — see Fraunhofer’s ROV-based underwater coating repair research.
The takeaway for surface preparation
A repair coating is only as durable as the surface it is applied to. RepaKORR’s field procedure shows why grit-free mechanical preparation — coating removal and profiling in a single step — is an established part of the offshore repair kit, especially where abrasive blasting cannot reach or cannot be used. More on marine and offshore surface preparation.
What the accelerated ageing tests showed
In a study presented in Nuremberg in April 2017, Fraunhofer IFAM and Muehlhan tested how surface preparation and the repair coating together decide how long a repair lasts. Steel panels with an "old" offshore system (2 × 300 µm epoxy plus an 80 µm acrylic-polyurethane topcoat), pre-damaged with delamination and steel corrosion, were prepared in three ways and recoated with a benchmark and three newly developed repair coatings.
| Surface preparation | Roughness Rz | Preparation grade | Panels |
|---|---|---|---|
| Grinding (electric, P60 corundum disc, 8,800 rpm) | 35 ± 4 µm | St 2 | 12 |
| Bristle Blaster® (electric, 2,200 rpm, no abrasive) | 53 ± 14 µm | Equivalent to Sa 2½ | 36 |
| Abrasive blasting (garnet 0.2–0.6 mm, 7 bar) | 81 ± 13 µm | Sa 2½ | 12 |
The repair coatings called for a roughness of at least Rz 30 µm (Rz 50 µm for the benchmark epoxy) and preparation to Sa 2½ or, for localised mechanical preparation, P Ma (ISO 8501-2). All panels were then aged according to ISO 20340: cycles of UV and condensation, neutral salt spray and temperature shock at −20 °C. Pull-off strength and rust creep from the damage were measured afterwards.
What the researchers concluded:
- Both the coating system and the surface preparation method had an extremely significant effect (p < 0.001) on pull-off strength and rust creep.
- For pull-off strength the two factors also interacted, and grinding changed the trends.
- The newly developed repair coating outperformed the benchmark on rust creep and pull-off strength, regardless of film thickness.
- Blast cleaning gave noticeably better performance, but is not always feasible offshore. Where it cannot be used, a higher film thickness is recommended.
Two practical points follow. First, grinding left a 35 µm profile at St 2, below the roughness the benchmark repair coating asks for; the Bristle Blaster® reached 53 µm at a grade equivalent to Sa 2½ without any abrasive. Second, in Muehlhan's own field procedure, "coating removal and profiling with rotating brush (Monti)" is the power-tool step used where blasting is not possible.
Why it matters
Offshore, a repair that fails early costs many times more than doing it right the first time. Choosing a preparation method that profiles, instead of one that only polishes, is prevention rather than cure. It keeps grit out of the sea, where blasting media cannot be contained (Planet), reduces the equipment and exposure needed for technicians at height and in the splash zone (People), and gives repair crews a method that independent research has measured (Power).
Frequently asked questions
What was the RepaKORR project?
RepaKORR was a German research project on repair systems and concepts for anticorrosive coatings on offshore wind structures. Funded by the Federal Ministry of Education and Research and coordinated by Muehlhan AG, it combined damage assessment, repair materials, application procedures, drone inspection and coating qualification by Fraunhofer IFAM.
Why do coatings on offshore wind structures fail?
RepaKORR’s analysis of platform-type structures attributed coating damage to mechanical damage (about 30%), unfavourable design (about 30%), insufficient coating (about 24%), welding (about 11%) and environment (about 5%). Much of it occurs at corners, openings, connections and poorly accessible areas, which are also hardest to repair.
Which tests were used to qualify the repair coatings?
Fraunhofer IFAM combined accelerated ageing with mechanical tests: falling-weight impact to ASTM G14, with more than 3.4 J for non-deck areas and more than 5.6 J for decks and boat-landing splash zones, and Taber abrasion to ASTM D4060, with less than 50 µm thickness loss per 1,000 cycles.
Where does bristle blasting fit in offshore coating repair?
In the power-tooling step, after washing and where wet blasting is impractical. A rotating bristle tool removes failed coating and creates an anchor profile in one grit-free step, which suits confined, access-limited and splash-zone areas worked from rope access. In hazardous areas a pneumatic, ATEX-evaluated tool is used.
This article summarises publicly presented research from the RepaKORR project for reference. MontiPower was not a formal project partner; MONTI rotating-brush tooling is shown in the project’s documented offshore application step.
Sources
- Fraunhofer-Gesellschaft, Long-lasting rust protection for offshore wind turbines (research news, February 2016). fraunhofer.de
- Muehlhan AG, Durable Coatings Offshore (presentation, 2016); Fraunhofer IFAM, accelerated ageing tests of offshore touch-up repair coatings (presentation). Project documents on file with MontiPower.
- ISO 12944-3:2017, Corrosion protection of steel structures by protective paint systems — Part 3: Design considerations. iso.org
- ASTM G14, Standard Test Method for Impact Resistance of Pipeline Coatings (Falling Weight Test). astm.org
- ASTM D4060, Standard Test Method for Abrasion Resistance of Organic Coatings by the Taber Abraser. astm.org